Precision requirements in aerospace manufacturing extend beyond the dimensions of an individual component. Complex contours, lightweight structures, difficult-to-machine alloys, traceable documentation, and tightly controlled inspection all influence how a part moves from engineering data to production.
For aerospace machined parts, the manufacturing plan needs to connect these factors rather than treating geometry, material, and quality as separate subjects. At Hanstar Technologies, we approach aerospace projects through this broader process view, with attention to both the technical requirements on the drawing and the information needed to maintain consistency across production.
Translate Complex Geometry Into A Machining Strategy
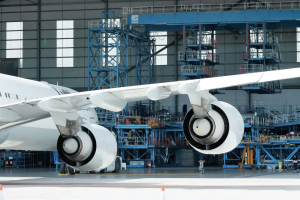
Aerospace components frequently contain curved surfaces, deep pockets, thin sections, angled features, and closely positioned interfaces. Such geometry can restrict tool access and make fixture orientation an important part of process planning. A feature that appears straightforward in CAD may require several tool orientations once cutter clearance, holder dimensions, and workholding are considered.
Five-axis machining can provide greater freedom around complex surfaces by changing the tool orientation during the cutting process. This can be particularly useful where multiple faces must maintain controlled spatial relationships. The machine configuration, however, should follow the geometry and tolerance requirements rather than being selected simply because additional axes are available.
Thin walls and deep cavities deserve special attention. Cutting forces can cause local movement, while long tools may introduce deflection or vibration. Designers and manufacturing teams can review wall proportions, internal radii, cavity depth, and feature accessibility together before releasing the production plan. Such early evaluation gives CNC machining for aerospace projects a clearer connection between design intent and practical machining conditions.
Select Materials With Machining Behavior In Mind
Material selection begins with application requirements, but manufacturing behavior also deserves consideration. Titanium offers a useful combination of strength and low density for many aerospace applications, while nickel-based superalloys such as Inconel are associated with demanding high-temperature environments. These materials do not behave identically during cutting, so the machining strategy needs to reflect their different thermal and mechanical characteristics.
Heat management can become especially important with difficult alloys. Titanium has relatively low thermal conductivity, which can concentrate heat around the cutting area. Inconel can retain strength at elevated temperatures and may place greater demands on tooling and cutting parameters. Tool selection, cutting speed, feed strategy, and chip evacuation all need to be considered alongside the part geometry.
Material documentation should remain connected to the released engineering package. The exact alloy or grade, material condition where applicable, and required certificates should be identified clearly rather than relying on broad descriptions. For aerospace machined parts, this information gives engineering, purchasing, quality, and manufacturing teams a shared material reference.
Build Quality Requirements Into The Workflow
Inspection planning should begin with the characteristics that matter to part function. Critical diameters, hole locations, profiles, flatness, positional relationships, and mating surfaces may require different measurement approaches. A drawing that identifies functional characteristics clearly gives the quality team a stronger basis for determining how those features should be verified.
Measurement equipment should correspond to the complexity of the component. Conventional instruments can handle many straightforward dimensions, while coordinate measuring machines can evaluate more intricate relationships between multiple features and surfaces. Inspection reports should also identify the relevant part number, revision, measurement results, and other traceability information required by the project.
Our aerospace machining work includes titanium, Inconel, and other high-temperature alloys on German Hermle five-axis machining centers. Critical features can be held to ±0.002 mm according to the applicable project requirements and verified using a Zeiss CONTURA CMM before shipment. We have supported eVTOL enterprises since 2020, producing flight-related hardware from one-off prototypes through production runs. These capabilities form part of our broader CNC machining for aerospace workflow rather than serving as standalone claims about any individual component.
Keep Documentation And Communication Synchronized
Technical communication becomes increasingly important as aerospace projects move between engineering, sourcing, quality, and manufacturing teams. A released CAD model should correspond with the correct drawing revision, while material specifications, inspection criteria, finishing requirements, and purchase-order notes should reference the same configuration. Unclear revision control can create questions that have little to do with machining itself but still affect production timing.
Supplier communication should also address unusual geometry before the order enters production. Deep features, narrow walls, complex profiles, difficult-to-access surfaces, and unusually tight tolerances may each influence setup planning or inspection. Discussing these characteristics early gives both sides an opportunity to clarify assumptions before they become manufacturing issues.
Quality-system information should be presented accurately and within its proper scope. Company-level certifications or documented quality procedures should not automatically be interpreted as certifications attached to an individual part. Clear communication keeps the distinction between manufacturing capability, quality-system controls, customer specifications, and part-level acceptance requirements visible throughout the project.
Conclusion
Aerospace machining becomes easier to manage when geometry, material behavior, inspection, documentation, and supplier communication are considered as one connected technical process. Deep pockets and complex contours may influence tool access, titanium and Inconel can change cutting conditions, while critical dimensions require an inspection approach suited to their function.
Our team at Hanstar Technologies combines German Hermle five-axis machining centers, Zeiss CONTURA CMM inspection, and experience with demanding aerospace materials to support projects from prototype quantities through production runs. Bring your drawings and specifications to us to discuss a practical CNC machining for aerospace manufacturing plan.