Moving from a finished drawing to a small production run involves more than sending a CAD file to a machine shop. Design validation, material selection, machining strategy, inspection requirements, and delivery planning all need to connect before production begins. Effective CNC prototyping gives engineering teams an opportunity to test dimensions, interfaces, assembly behavior, and functional details before committing to a larger manufacturing program.
At Hanstar Technologies, we approach this transition by combining engineering review with practical machining considerations, helping teams turn validated designs into workable low-volume production plans.
Start With Design And Manufacturability
The drawing should be treated as the starting point for a manufacturing discussion rather than an isolated specification. Wall thickness, hole depth, internal corners, thread locations, tolerances, and surface requirements can all influence machining time and tooling decisions. A design that performs well in a digital model may still require modification to accommodate real cutting tools or inspection access.
DFM analysis is especially useful before the prototype reaches the machine. Engineers can identify features that create unnecessary setup operations, difficult tool paths, or excessive material removal. Addressing such issues early can make the transition from CNC prototyping to repeat production more predictable without changing the functional purpose of the part.
Tolerance strategy deserves similar attention. Not every dimension needs the same degree of precision, and applying unnecessarily tight tolerances throughout a component can increase manufacturing complexity. Critical interfaces should be identified first, followed by functional dimensions, cosmetic features, and less sensitive areas.
Select The Right Process And Material
Process selection depends on geometry, quantity, material, dimensional requirements, and expected production frequency. CNC milling works well for many prismatic components and complex surfaces, while CNC turning is suited to rotational parts such as shafts, bushings, and threaded cylindrical components. Some projects may require multiple operations to produce one finished part.
Material decisions should come from the component’s actual operating environment. Aluminum may be suitable where low weight and machinability matter, while stainless steel can serve applications requiring greater corrosion resistance and mechanical strength. Engineering plastics may provide useful combinations of low density, electrical insulation, or chemical resistance in specific applications.
Prototype quantities can sometimes justify a different process from later production volumes. A low-volume program may stay with CNC machining because tooling investment is limited and design changes remain manageable. Material availability should also be checked early, since uncommon grades or specific certification requirements can affect procurement schedules.
Build Inspection Into The Production Plan
Inspection should not begin only after machining is finished. Critical dimensions need measurable definitions in the drawing, and the inspection method should match the required accuracy. Calipers and micrometers may handle straightforward dimensions, while coordinate measuring machines can provide more detailed dimensional verification across complex geometries.
A sensible inspection plan separates critical characteristics from routine checks. Hole position, mating surfaces, concentricity, flatness, or other functional features may deserve tighter control than non-critical exterior dimensions. Recording these priorities helps production and quality teams focus resources where dimensional variation matters most.
For teams working with a precision parts manufacturer, inspection documentation can also become part of supplier coordination. First-article reports, dimensional records, material certificates, and agreed acceptance criteria create a common reference between engineering and manufacturing. Such records become particularly valuable when a prototype transitions into recurring low-volume orders.
Coordinate Production And Supply
Low-volume manufacturing still requires supply-chain planning. Material purchasing, machining capacity, finishing services, inspection time, packaging, and shipping can each affect the final delivery schedule. Treating these activities as separate tasks may create gaps between one stage and the next.
Production quantities should be discussed alongside expected order frequency. A customer might need fifty components immediately and another fifty several months later, creating different capacity and inventory considerations from a single 100-piece shipment. Forecast information can help suppliers prepare material and machining resources more effectively.
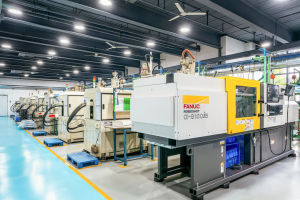
At Hanstar Technologies, our custom manufacturing service combines high-precision CNC equipment, senior engineering support, DFM analysis, and full-cycle quality inspection for custom metal and plastic components. Our CNC turning capabilities are suited to tight-tolerance parts, while engineering review helps connect the original design with practical machining requirements. This integrated approach is particularly relevant to programs that need both prototype validation and subsequent small-batch production.
Prepare For Repeatable Low-Volume Production
Prototype approval should trigger a second engineering review rather than mark the end of technical work. Once the design has been validated, teams can examine setup requirements, fixture concepts, tooling arrangements, inspection frequency, and production documentation. These details help convert an individual prototype into a repeatable manufacturing process.
Revision control becomes increasingly important at this stage. Changes to hole dimensions, material grades, finishes, or tolerances should be reflected consistently across drawings, CAD files, purchase orders, and inspection documents. Clear version identification prevents older specifications from remaining in circulation.
Communication should continue after the first production batch. Dimensional results, machining observations, material availability, and delivery performance can reveal opportunities to refine future orders. A well-managed program treats each batch as part of an ongoing manufacturing relationship rather than as an isolated transaction.
Conclusion
Turning a validated design into low-volume production works best as a connected sequence: review the geometry, assess manufacturability, select suitable materials and processes, define inspection requirements, then coordinate capacity and supply before repeat orders begin. CNC prototyping provides valuable evidence during the early stage, while disciplined production planning carries that knowledge into subsequent batches.
At Hanstar Technologies, we support this progression with precision machining, engineering-led DFM analysis, and full-cycle quality inspection for custom components. If your next project needs a practical path from prototype to low-volume manufacturing, our team is ready to discuss the drawings, production requirements, and inspection expectations with you.