A procurement program becomes harder to manage once different components require different production methods, materials and quality criteria. The practical challenge is not simply finding a source for each individual part; it is understanding why one geometry belongs on a CNC machine while another is better suited to molding, die casting or sheet-metal forming.
Custom part manufacturing provides a framework for connecting those decisions to actual product requirements. At Hanstar Technologies, we approach this process by looking at geometry, material, quantity and function together, giving engineering and sourcing teams a clearer basis for planning a multi-process program.
Start With Geometry And Function
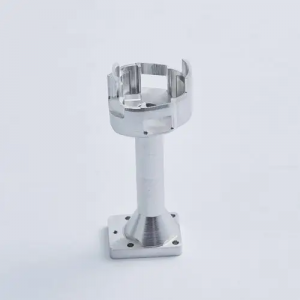
Geometry provides the first useful indication of which manufacturing route may fit a component. CNC machining works from solid stock and can produce pockets, bores, contours and closely controlled interfaces. Molding becomes more relevant when a part has repeated three-dimensional geometry and projected volumes can support tooling investment. Sheet metal, meanwhile, suits designs built around flat profiles, bends, flanges and formed structures.
Functional requirements add another dimension to the assessment. A mounting bracket may need stiffness and accurate hole locations, while an enclosure could prioritize folded geometry, internal clearance and accessible fastening points. A component used as a mechanical interface may demand localized machining even if its primary structure comes from another process.
Rather than assigning a process based on appearance alone, procurement teams can map each critical feature to the operation that creates it. This makes precision parts manufacturer evaluation more meaningful because capability is considered in relation to the actual part instead of a broad equipment list.
Match Materials To Manufacturing Methods
Material selection can significantly influence process suitability. Aluminum, stainless steel and engineering plastics behave differently during cutting, forming, molding and finishing. Mechanical strength, thermal performance, corrosion resistance, conductivity and operating temperature should all be considered before the production route is fixed.
Injection molding may be attractive for polymer components with intricate repeated geometry, particularly once production quantities make tooling economics practical. Die casting can serve metal parts where complex shapes and higher production volumes justify dedicated dies. CNC machining remains useful for materials and geometries that require controlled material removal, while sheet fabrication can efficiently create structures from relatively thin stock.
Quantity changes the material-process relationship as well. Prototype quantities may favor flexible production methods with modest tooling commitments, whereas recurring demand can shift attention toward cycle time, cavity count, material utilization and automation. Well-planned custom part manufacturing considers these variables before procurement decisions become tied to a single process.
Connect Volume With Production Economics
Production quantity should be viewed as more than an annual forecast. Procurement teams also need to consider release frequency, batch size, expected product life and the likelihood of engineering changes. A component ordered several times per year may have very different manufacturing economics from one produced continuously.
Tooling is particularly important for molding and die casting. Initial investment can represent a substantial portion of early project cost, while the cost profile per unit may change as production volume increases. CNC machining and sheet fabrication can offer different cost structures because they generally rely less heavily on dedicated forming tools.
Program planning becomes easier when teams compare the total manufacturing route rather than one quotation line. Material, tooling, machining, finishing, inspection, packaging and logistics can all affect the delivered component cost. These considerations also help procurement teams determine what information a precision parts manufacturer needs before preparing a realistic production proposal.
Coordinate Secondary Operations And Quality
The primary process rarely defines the finished component by itself. CNC post-machining may refine holes or mating surfaces on cast parts, while fabricated sheet components may require deburring, coating or additional forming. Molded parts can also involve trimming, inserts or other secondary operations depending on the design.
Quality planning should follow the functional importance of each feature. Critical dimensions, assembly interfaces and sealing surfaces may require more detailed inspection than non-functional areas. Defining those requirements early gives manufacturing and quality teams a common reference for production checks.
Documentation matters across multi-process programs because different operations can affect the same component. Inspection results, material records, drawing revisions and process information need to remain connected to the applicable part revision. Strong custom part manufacturing programs treat quality information as part of the production workflow rather than as paperwork added after fabrication.
Build One Connected Manufacturing Workflow
A multi-process supplier becomes more useful when engineering information can move between production stages without being recreated from scratch. DFM review can identify geometry concerns early, material inspection can verify incoming stock or resin, and fabrication can follow the approved technical requirements. This sequence creates a more connected path from drawing review to physical production.
Our end-to-end manufacturing workflow at Hanstar Technologies includes DFM design review, incoming raw-material inspection and precision fabrication across CNC machining, die casting, injection molding and sheet-metal forming. We can assess the design before production, review material requirements and then apply the relevant fabrication method according to the component’s geometry and program needs.
Conclusion
Different manufacturing technologies solve different production problems, and the most practical program usually reflects those differences rather than ignoring them. Geometry determines how a part can be formed or machined, material influences process behavior, volume shapes the economics, and function establishes which dimensions and operations matter most. Precision parts manufacturer selection becomes more useful when these factors are considered as one connected decision rather than separate purchasing criteria.
With custom part manufacturing capabilities spanning several fabrication methods, Hanstar Technologies can work with engineering and procurement teams to assess individual components within the broader production program. Send us your drawings, material specifications and projected quantities to discuss the appropriate manufacturing route.